Release PET Film for Split-Back Liners
Nov 14,2026 | FOSHAN CAILONG METALLIC PACKAGING MATERIAL CO.,LTD
A split liner lets an installer expose a small area of adhesive first, align the part, and then remove the rest of the backing. The process becomes unreliable if the first half pulls the second half with it or if the part shifts when the second half is removed. Buyers evaluating release PET film should check the complete adhesive-backed part in the intended installation sequence. An even peel from an uncut strip does not show how the liner behaves at the split or where an installer takes hold of the tab.
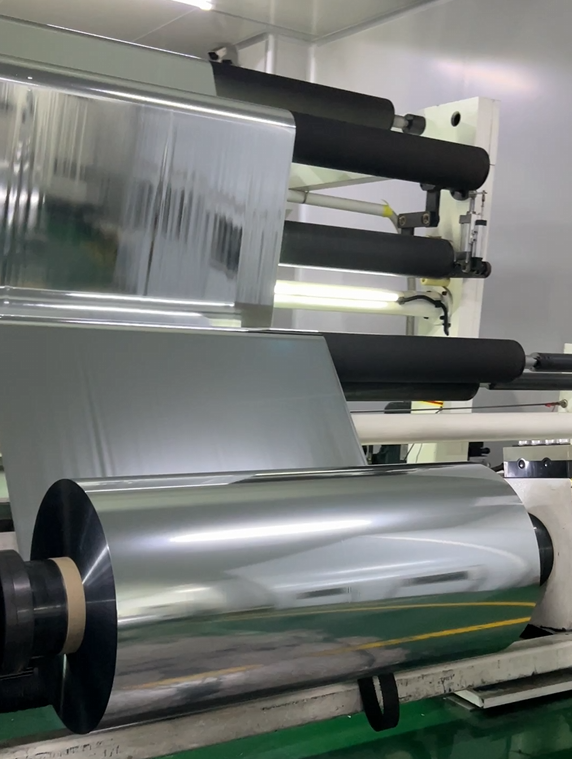
Cailong's film portfolio lists silicone-coated PET release film with a smooth surface and low adhesion. Ask the supplier to identify the release side and the offered release level for the intended adhesive. Keep the adhesive, face stock and storage history with the trial record. The film is one part of the release system, and the two liner sections also depend on the design and quality of the cut.
Decide what each liner half has to do
Draw the part as the installer receives it. Mark the first pull tab, the first exposed adhesive region and the point where the second liner half becomes accessible. Show whether the initial exposed area is meant to hold a temporary alignment or become a permanent bond immediately. Record the angle and direction in which the installer can pull in the available space. A split that is easy to reach on a bench may sit against a wall in the installed position.
Agree where the liner split should lie relative to the placement datum. If an installer anchors a small strip first, check the width of that strip after converting. A split that falls too close to the edge can leave too little area to hold the position. A split too far inboard can expose adhesive before the part is aligned. Include these conditions when deciding what the converter needs to measure.
Inspect the cut without disturbing the adhesive
Keep samples from the start and stable portion of the converting run. Inspect the split line with the part supported as it would be before installation. Look for areas where the liner remains connected or where the part below appears marked. Where an approved inspection method is available, use it to assess the cut depth. A cut that does not fully separate the liner can pull both halves together, while a cut that reaches too far may mark the underlying construction.
Check the end of the split where the installer begins pulling. Record the shape and accessibility of the tabs and note whether the edges lift while packed. Include the normal stacking arrangement and observe samples after the expected transport or storage interval. A tab that is easy to find on a newly cut piece can be flattened or obstructed by neighboring parts. Preserve a sample of the package layout if that contact matters.
Run the actual two-step installation
Prepare the intended substrate according to the approved process and use the production part dimensions. Remove the first half as specified, place the part and note whether the second half stays attached and easy to reach. Mark the initial alignment relative to the assembly reference. Then pull the second half and inspect the final position. If the part moves, record the direction and the stage of removal rather than reporting only its final offset.
Observe the surface as the liner releases near the split and across the last part of the peel. Look for adhesive lifting, a fold that traps the liner or a sudden jump that changes the position of the part. If the liner is difficult to remove at one spot, preserve both surfaces for the converter. The defect may follow the cut or local contact rather than the nominal release property of the full roll.
Compare release evidence at the right stages
If a release measurement is part of approval, identify the adhesive, dwell, conditioning, specimen width and test geometry used. Record results for the relevant regions before and after aging where required. Keep these results separate from the practical installation observations. A uniform laboratory peel can be useful for monitoring material supply, while the assembly trial can show whether an operator can complete the intended sequence without moving the part.
If the problem appears only with the second half, compare the peel path on an installed piece with an uninstalled reference. The first bonded section changes how much the part can flex and the direction in which the liner is pulled. An adjustment to tab placement or split direction may change that behavior without requiring a different release level. Keep such geometry changes identified during the comparison.
Specify what the converter must deliver
Send the desired PET liner gauge, release side, adhesive system and supply width to the material supplier. Give the converter the split location, tab dimensions and inspection requirements. Include the actual order of liner removal and any installation constraints. If the quote covers film only, confirm who will carry out the split and verify it on the production construction.
Retain an uninstalled part, a reference installed part and the two removed halves from an accepted trial. If a later order changes adhesive, storage interval or cut tooling, review the affected stage before using the previous approval. Tie the liner specification to the assembly result and the measured release requirement so a repeat order can reproduce both.
Where left-handed and right-handed installations use mirror-image parts, check both versions with their own tab positions. The release film can remain the same while the available pull direction changes. Label each accepted version on the installation sheet to avoid applying one result to the other.
Comment